Project Case Studies
These five projects are drawn from our own records, ranging from a power-plant screen in Gujarat to a temple gopuram on the Karnataka coast. Each case study presents the scope, duration and team and, where the client provided one, the completion letter.
- Essar Projects / Essar Heavy Engineering ServicesHazira, Gujarat, 2013Zinc metallizing on a power-plant coarse screen, completed in 100 days.
- Chettinad Cement CorporationAriyalur, Tamil Nadu, 2012Blasting and aluminizing of a cement-plant RABH chimney in 15 days.
- Engineers India LtdPadur, Udupi district, Karnataka, 2013Thermal spray aluminium coating on a strategic crude oil storage project.
- Prakash Asphaltings & Toll HighwaysState Highway 27, Ratlam, Madhya Pradesh, 2011Aluminizing and three coats of paint on 2,600 m² of railway bridge girders.
- Murudeshwara TrustMurudeshwara, coastal Karnataka, 2004Abrasive blasting and aluminizing of a statue and temple gopuram on the Karnataka coast.
Power Plant Coarse Screen, Hazira
- Client
- Essar Projects / Essar Heavy Engineering Services
- Location
- Hazira, Gujarat
- Year
- 2013
- Scope
- Zinc metallizing, coarse screen of a power plant
- Duration
- 100 days (7 Jul to 14 Oct 2013)
- Team
- 20 people
The asset and why it needed protection
Context: a coarse screen in a power plant is a large steel structure that operates in a wet, harsh environment and is difficult to take out of service for recoating. Bare or thinly painted steel in such conditions begins to rust early.
Zinc metallizing is applied cold, so there is no limit on component size and no heat distortion, and the zinc continues to protect the steel even where the coating is scratched. For this reason it is a common choice for large structural steel.
Work Carried Out by Mythri Metallizing
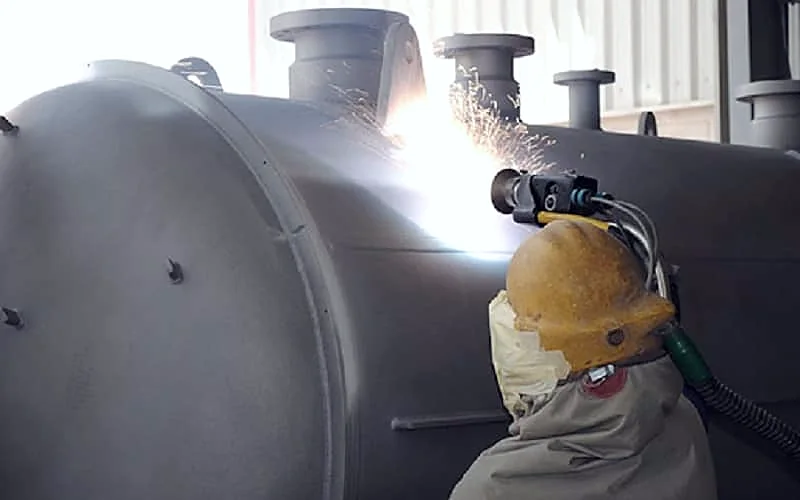
Work commenced on 7 July 2013 and was completed on 14 October 2013, a period of 100 days. Mythri Metallizing mobilised manpower, equipment and raw material to the Hazira site, and a team of 20 carried out the work. The standard sequence for zinc metallizing is as follows:
Blasting
The steel is abrasive blasted to near-white metal (Sa 2½) so that the zinc can grip the surface profile.
Spraying
Zinc wire is arc or flame sprayed onto the blasted steel in even, overlapping passes.
Sealing and painting
The zinc is sealed, and paint is applied where the specification requires it.
Testing
Coating thickness is measured with a calibrated gauge and the readings are recorded.
“Completed metalizing within the schedule time.”
Essar, letter dated 5 September 2014
“The quality of their workmanship was excellent.”
Essar, letter dated 5 September 2014
“Resourceful, competent and very co-operative at our project site.”
Essar, letter dated 5 September 2014
- Related processes:
- Thermal spray zinc
- Abrasive blasting
- Flame spray
RABH Chimney, Ariyalur
- Client
- Chettinad Cement Corporation
- Location
- Ariyalur, Tamil Nadu
- Year
- 2012
- Scope
- Blasting and aluminizing of the RABH chimney
- Duration
- 15 days
- Team
- 15 people
The asset and why it needed protection
Context: an RABH (reverse air bag house) chimney in a cement plant carries hot, dusty flue gas. Heat and acidic condensate cause ordinary paint to fail early on such steel.
Aluminium resists oxidation and corrosion at temperatures where most paints soften. A properly applied and sealed aluminium coating is expected to last 10 years or more.
Work Carried Out by Mythri Metallizing
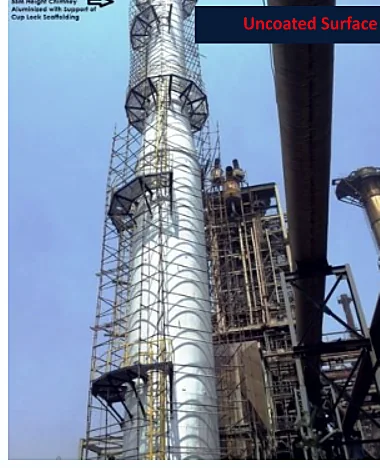
Mythri Metallizing blasted and aluminized the chimney in 15 days with a team of 15. The standard sequence for aluminizing is as follows:
Blasting
The steel is abrasive blasted to white or near-white metal and the surface profile is checked.
Spraying
Aluminium wire of 99.5% purity is arc sprayed in crossing passes to an even thickness.
Sealing
A sealer is applied to close the pores of the sprayed layer.
Testing
Thickness is gauged, adhesion is tested and the results are retained in the project record.
“Entirely to our satisfaction in terms of speed, quality and workmanship.”
Chettinad Cement Corporation
- Related processes:
- Thermal spray aluminium
- Abrasive blasting
- Grit blasting
ISPRL Crude Oil Storage, Padur
- Client
- Engineers India Ltd (ISPRL strategic crude oil storage)
- Location
- Padur, Udupi district, Karnataka
- Year
- 2013
- Scope
- Thermal spray aluminium coating (TSAC)
- Duration
- About 6 months
- Team
- 45 people
The asset and why it needed protection
Context: crude oil storage is long-life infrastructure that owners intend to keep in service for decades, with minimal shutdown for repainting. Udupi district lies on the Karnataka coast, where humid, salt-laden air attacks bare steel.
Thermal spray aluminium provides a barrier that performs well in marine and industrial air, and in chloride conditions it also protects the steel sacrificially.
Work Carried Out by Mythri Metallizing
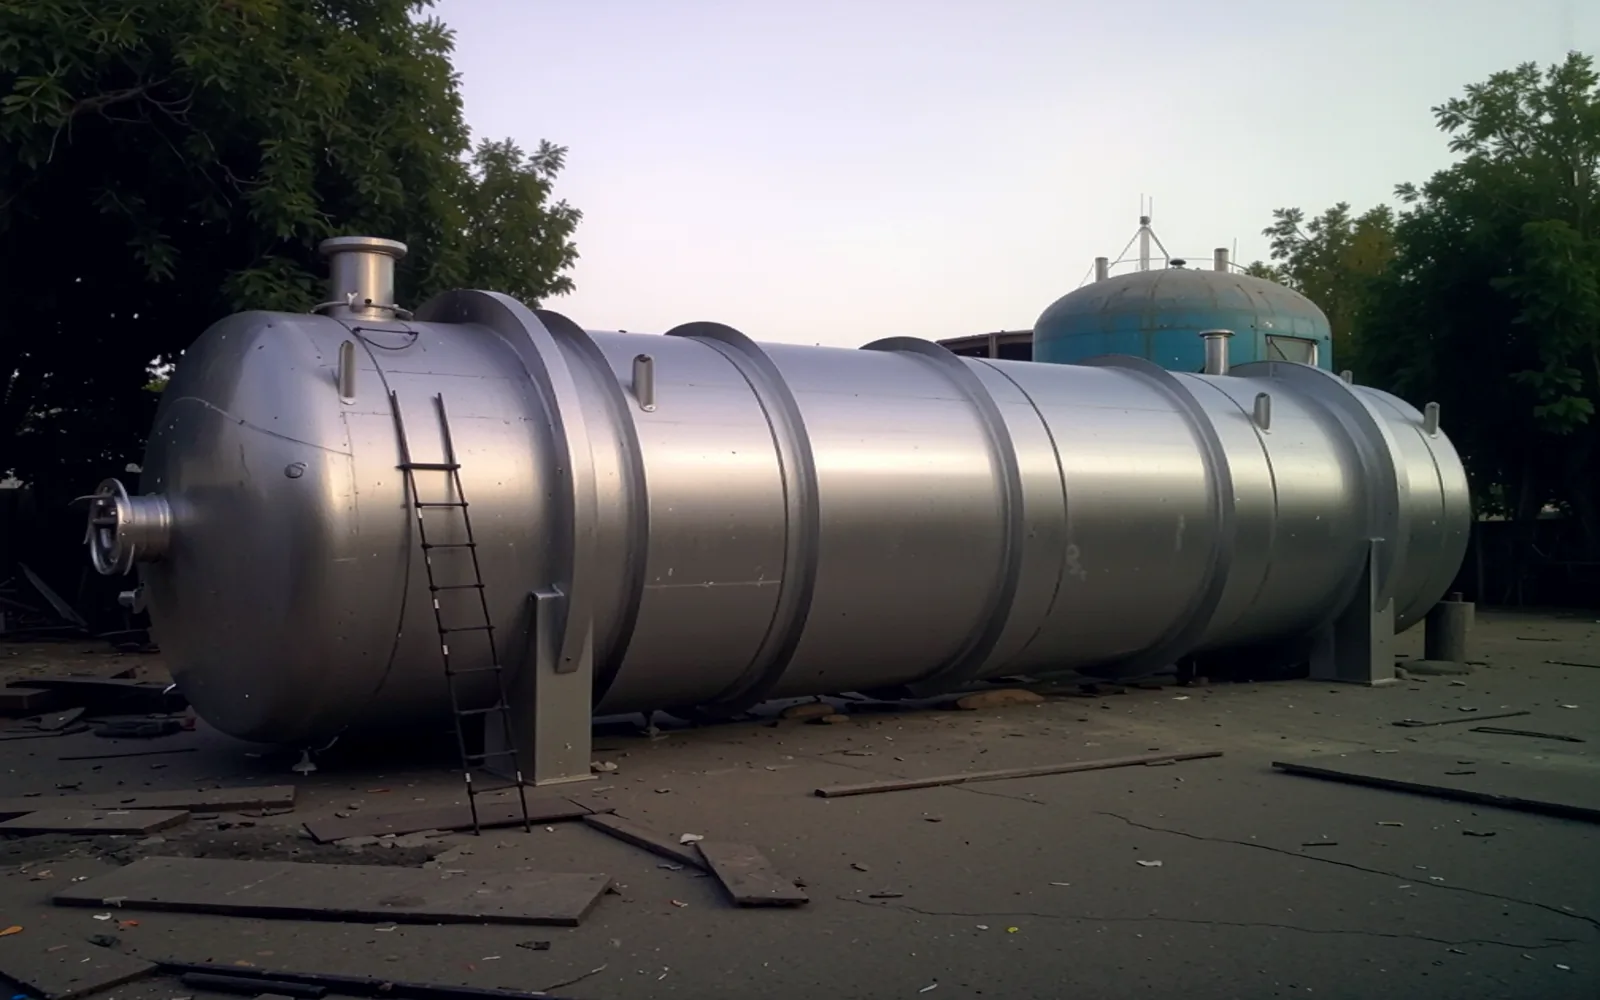
The letter of Engineers India Ltd dated 6 February 2013 approved Mythri Metallizing as the TSAC applicator for the project. The work took about 6 months and was carried out by a team of 45. The standard sequence for TSAC is as follows:
Blasting
The steel is abrasive blasted to white or near-white metal, and the profile is checked before spraying.
Spraying
Aluminium is arc sprayed onto the freshly blasted steel to the specified thickness.
Sealing
The pores of the coating are closed with a sealer, and paint is added where specified.
Testing
Thickness and adhesion are measured and the results are recorded.
- Related processes:
- Thermal spray aluminium
- Coating sealing
- Abrasive blasting
Railway Bridge Girders, Ratlam
- Client
- Prakash Asphaltings & Toll Highways (India) Ltd
- Location
- State Highway 27, Ratlam, Madhya Pradesh
- Year
- 2011
- Scope
- Metallizing (aluminizing) and 3 coats of paint on 2,600 m² of steel girders
- Duration
- About 1 month
- Team
- 10 people
The asset and why it needed protection
Context: bridge girders are exposed to rain, sun and pollution, and repainting them requires working at height and, on a railway bridge, close to live traffic. A durable system applied once avoids repeated access.
A metallized layer beneath the paint provides sacrificial or barrier protection if the paint is damaged, and extends the life of the paint above it.
Work Carried Out by Mythri Metallizing
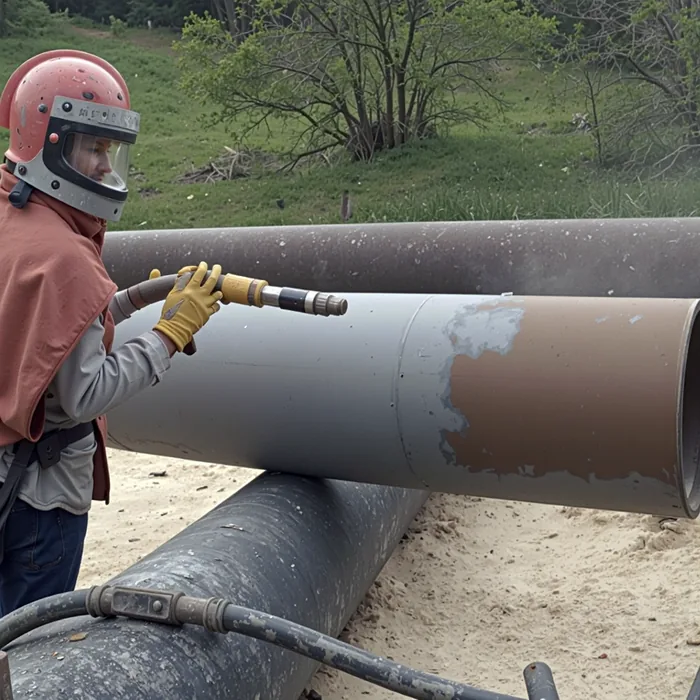
Mythri Metallizing metallized (aluminized) and applied 3 coats of paint to 2,600 m² of steel girders, as per Indian Railway Standard specifications. The work took about 1 month with a team of 10. The standard sequence is as follows:
Blasting
The girders are abrasive blasted to near-white metal.
Spraying
Aluminium is arc sprayed onto the blasted steel.
Sealing and painting
The coating is sealed and the paint coats are applied, three on this project.
Testing
Thickness is gauged and the readings are recorded.
“Completed Metalizing within the scheduled time.”
Prakash Asphaltings & Toll Highways (India) Ltd, letter dated 11 June 2011
“Quality of their workmanship was excellent.”
Prakash Asphaltings & Toll Highways (India) Ltd, letter dated 11 June 2011
“Resourceful, competent and very co-operative at our project site.”
Prakash Asphaltings & Toll Highways (India) Ltd, letter dated 11 June 2011
- Related processes:
- Thermal spray aluminium
- Industrial spray painting
- Abrasive blasting
Lord Shiva Statue, Murudeshwara
- Client
- Murudeshwara Trust
- Location
- Murudeshwara, coastal Karnataka
- Year
- 2004
- Scope
- Abrasive blasting and aluminizing of the Lord Shiva statue and the temple gopuram
- Duration
- About 6 months
- Team
- 30 people
The asset and why it needed protection
Context: steel and metal structures on the coast stand in humid, salt-bearing air, which accelerates rusting. Large monuments cannot be taken down for repair, so protection must be applied on site.
Aluminium coatings perform well in marine air, which is why aluminizing is used on coastal steel.
Work Carried Out by Mythri Metallizing
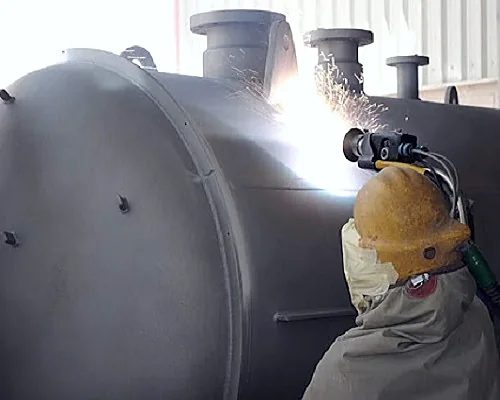
Mythri Metallizing abrasive blasted and aluminized the Lord Shiva statue and the temple gopuram. The work took about 6 months with a team of 30. The standard sequence is as follows:
Blasting
The surface is abrasive blasted back to clean, bright metal.
Spraying
Aluminium is arc sprayed onto the freshly blasted surface.
Sealing
The coating is sealed to close its pores.
Testing
The coating thickness is gauged and recorded.
- Related processes:
- Thermal spray aluminium
- Abrasive blasting
- Thermal spray zinc
Discuss a Similar Structure
Please share the drawing, the size and the site, and one of our engineers will respond with a coating specification.
- Reply within one working day
- Drawings kept confidential
- Email acknowledgement
Thank you. Your enquiry has been received.
One of our engineers will contact you to discuss the requirement. A confirmation has been sent to your email address.