Stress Relieving Services
Controlled furnace cycles for fabrications and castings, up to 30 t and 900 °C.
- Since 2004
- Up to 30 tonnes, 900 °C max
- Printed temperature record
Why Stress Relieving Is Essential
When steel is welded, cast or heavily machined, it cools unevenly and stresses are locked into it. If left in place, these stresses can cause a part to move when it is machined, to distort over time, or to crack in service, especially under fatigue or in corrosive conditions.
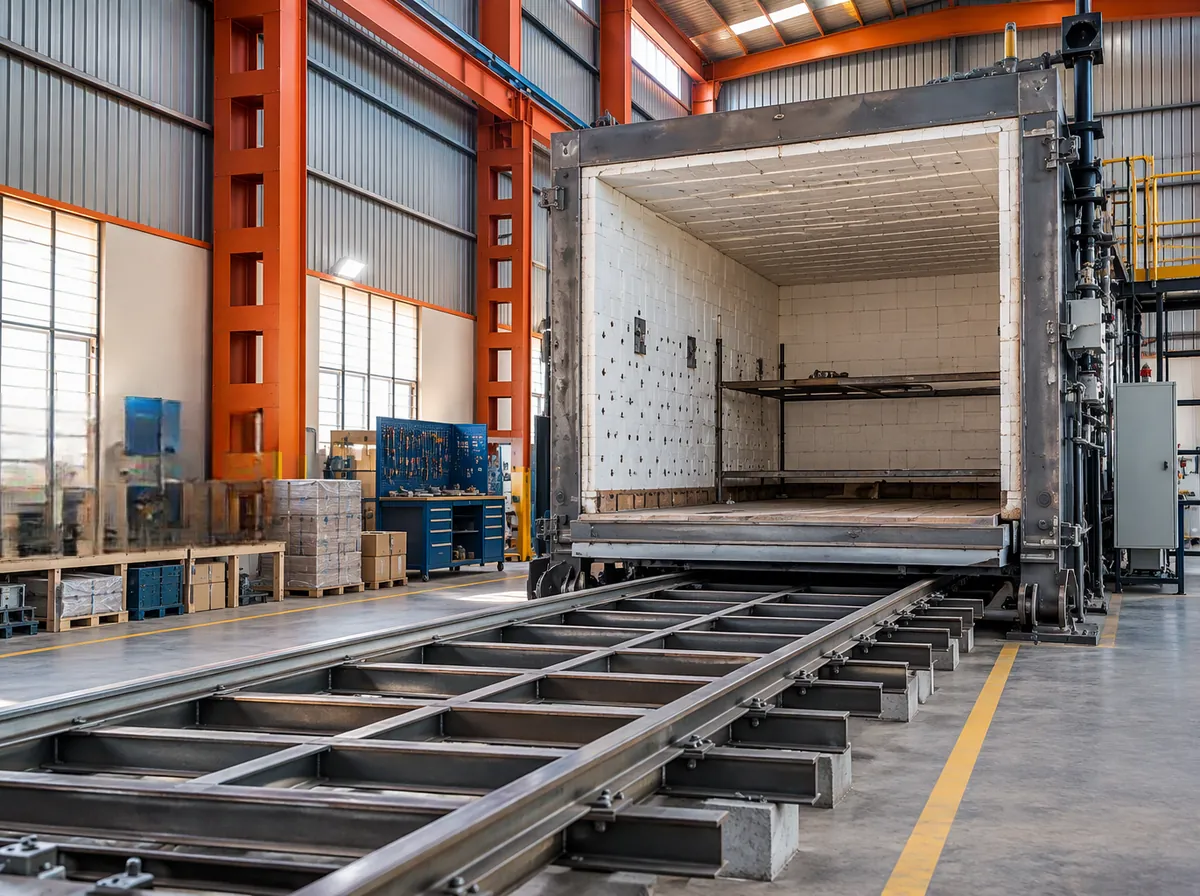
Stress relieving heats the whole part slowly to a temperature well below the point at which its structure changes, holds it there long enough for the stresses to relax, and then cools it slowly and evenly. The part emerges dimensionally stable, with its strength intact.
Mythri Metallizing added stress relieving in 2004. Our furnaces handle fabricated machine bases and castings that must hold their accuracy after machining, as well as welded fabrications for engineering and process plants.
When a Part Should Be Stress Relieved
Before Precision Machining
Machine-tool beds, bases and columns that must not move after they are machined.
After Heavy Welding
Thick or highly restrained weldments, where residual stress is highest.
Castings
Steel and cast iron castings with uneven sections that cooled at different rates.
When the Drawing or Code Requires It
Post-weld heat treatment specified on the drawing or by the applicable code.
Specification
The cycle is set from your drawing, code or material. For a part close to the size or weight limit, please share the drawing with us in advance.
- Furnace capacity
- Up to 7 m long, 3.5 m wide and 3 m high
- Maximum load
- Up to 30 tonnes
- Maximum temperature
- 900 °C
- Heating
- Oil-fired burners with blowers
- Temperature control
- Type K (chromel-alumel) thermocouples; digital indicator and recorder with printer
- Loading
- Rail-mounted furnace trolley with drive motor, and crane handling
- Typical parts
- Welded fabrications, machine-tool bases and castings
- Materials
- Carbon and low-alloy steels, cast iron
- Cycle
- Heating rate, soak temperature and time, and cooling rate agreed for each project
- Follow-on
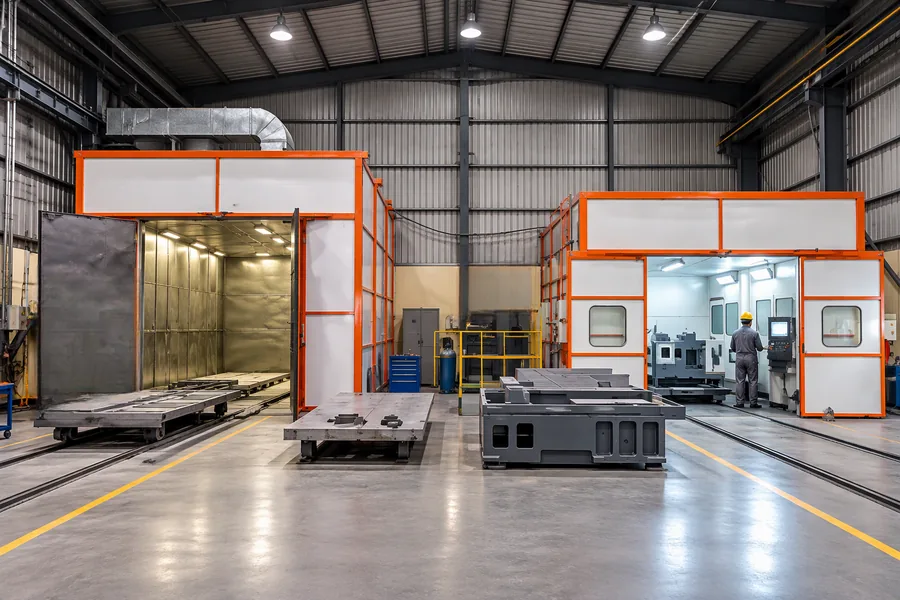
- Blasting, primer and paint in the same unit
Process Steps
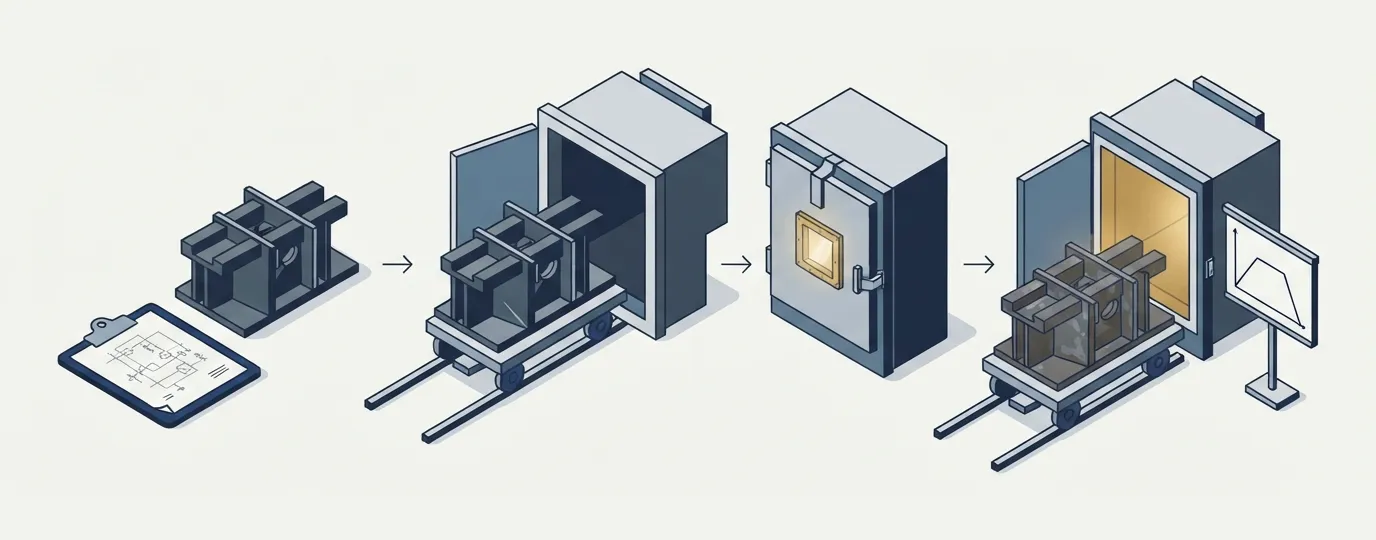
Review the Drawing
We confirm the material, thickness and required cycle, from your drawing or code or from our recommendation.
Load
Parts are placed on the furnace car and supported so that they cannot sag as they heat.
Heat and Soak
The furnace brings the load up at a controlled rate and holds it at temperature for the soak time.
Cool and Unload
The load cools at a controlled rate before it is removed, ready for blasting and painting if required.
Applications
We stress relieve for machine-tool builders, fabricators and engineering manufacturers around Bengaluru.
- Machine-tool beds, bases and columns
- Welded fabrications and frames
- Steel and cast iron castings
- Structural assemblies before machining
- Dies and fixtures
Frequently Asked Questions
At what temperature is stress relieving carried out?
What is the largest part that can be stress relieved?
Is a record of the heat treatment cycle provided?
Will stress relieving distort the part?
Can the parts be blasted and painted afterwards?
Is there a minimum quantity?
Get a Stress Relieving Quote
Share the drawing, the material and the weight of the part. We will confirm the furnace cycle and reply with a quotation.
- Reply within one working day
- Drawings kept confidential
- Email acknowledgement
Thank you. Your enquiry has been received.
One of our engineers will contact you to discuss the requirement. A confirmation has been sent to your email address.