Corrosion Protection in Hyderabad
Steel in Hyderabad plants is attacked mainly by process fumes and heat rather than by sea air.
- Blast, metallize, seal, paint
- Zinc or aluminium, 175–200 µm
- Test reports with every project
Coatings for Fumes, Spills and Heat
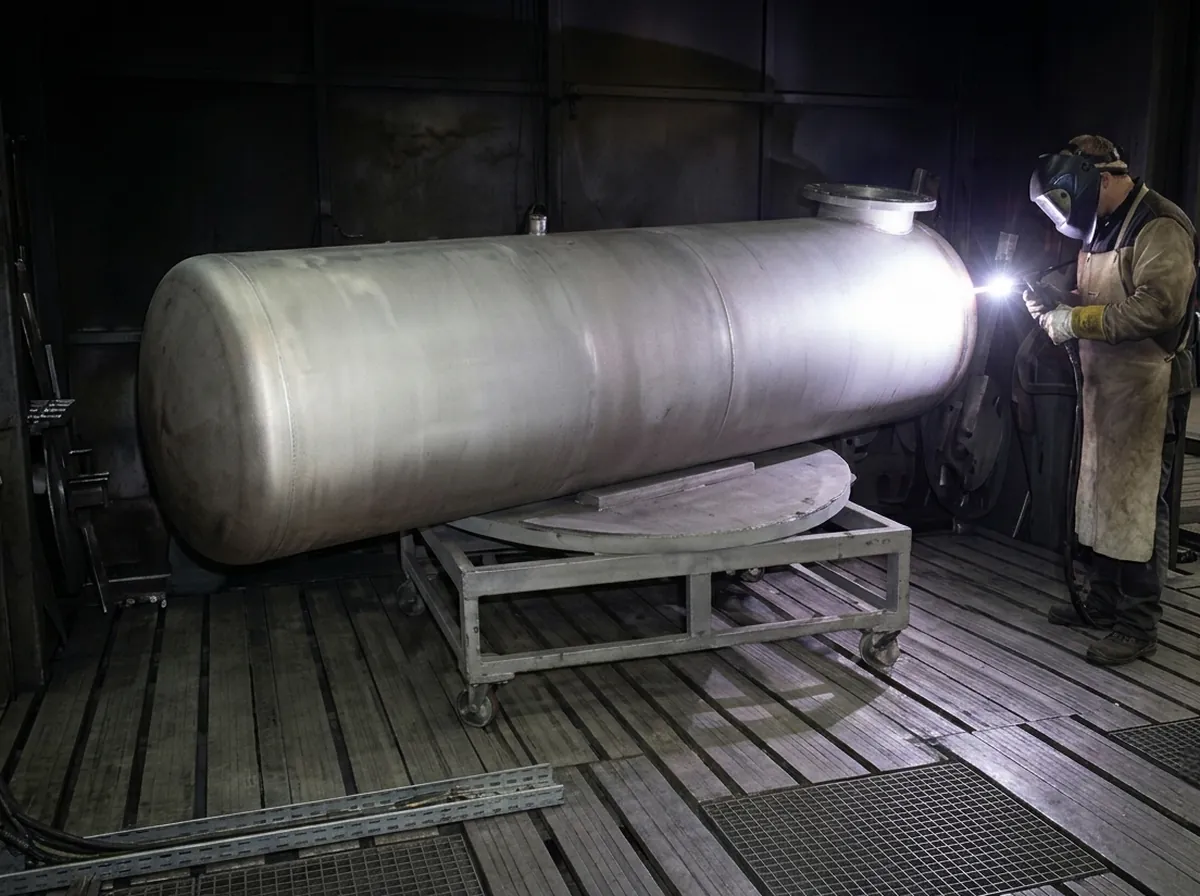
Hyderabad is an inland city, and hot and dry for much of the year. Corrosion in its pharma, bulk drug and chemical zones is driven by the process atmosphere, which includes acid and solvent vapours, washdown water and spills. Heat from boilers, stacks and hot pipework adds to the effect.
The coating system must therefore be chosen for that atmosphere. Thermal spray zinc suits most outdoor structural steel, while thermal spray aluminium is the better choice for hot surfaces, stacks and chemical service. Neither metal alone is a barrier against strong acid or alkali splash, so where spills are likely we add a sealer and a paint topcoat selected for the chemical.
Where steel is not exposed to heat or direct fumes, a blasted and painted system may be sufficient. We apply the system that your consultant or paint supplier specifies, and we will advise you when metallizing is not required.
Applications Around Hyderabad
Bulk drug and chemical plants
Patancheru, Pashamylaram, IDA Bollaram and Jeedimetla. Pipe racks, tank and reactor supports and utility structures exposed to fumes, washdown and spills.
Boiler houses, stacks and DG sets
Chimneys and hot ducting at pharma, chemical and power sites, where thermal spray aluminium is the usual answer to heat. We have aluminized chimneys in Gujarat, Tamil Nadu and Karnataka.
Power equipment and heavy fabrication
Structures and equipment from the Ramachandrapuram, Balanagar and Medchal belts, coated in the fabrication yard or at the erection site. Zinc suits most structural steel.
Defence, aerospace and engineering manufacturing
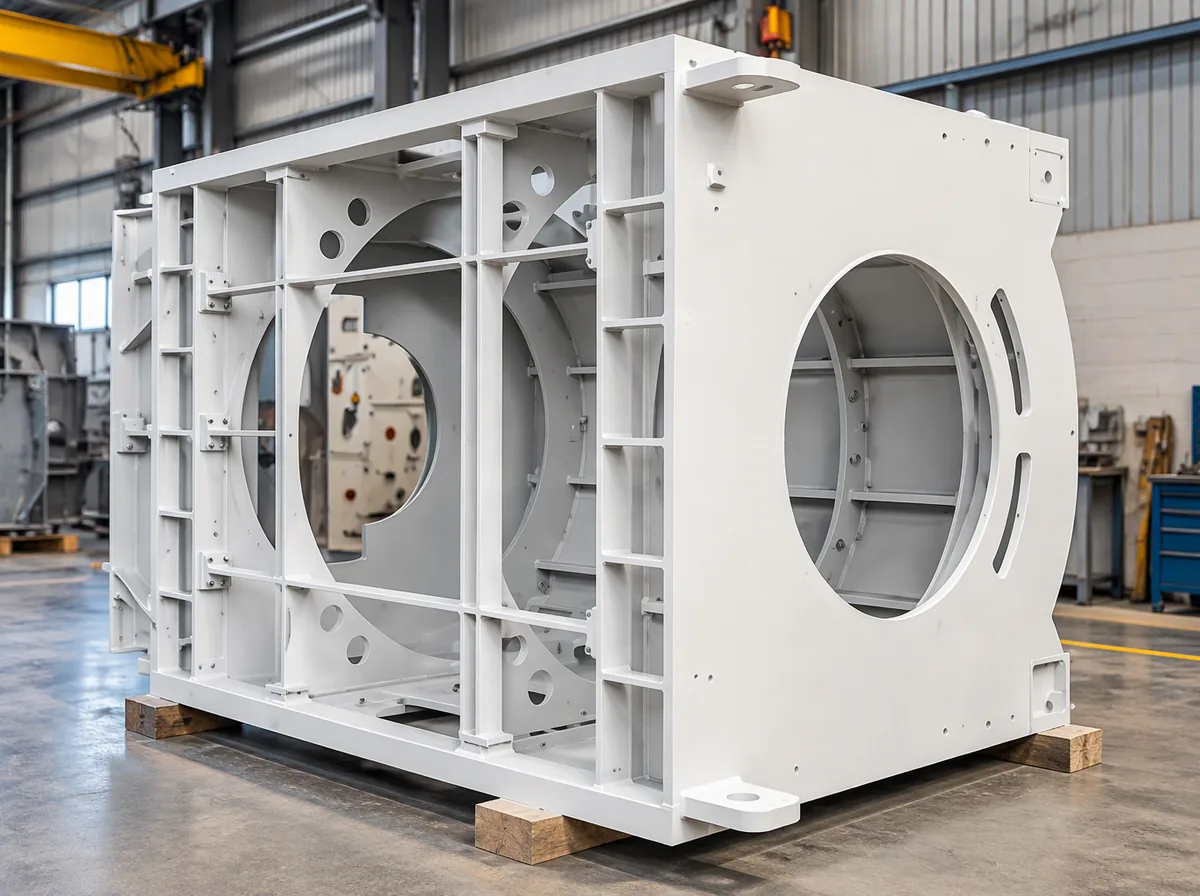
Equipment bases, fixtures and enclosures that require a documented coating. Surface profile, thickness and adhesion results are recorded and supplied as a test report.
One System, One Crew, One Visit
A full system proceeds in sequence: blasting to Sa 2½ or Sa 3, zinc or aluminium spray at 175–200 µm, application of the sealer, and then paint where specified. Metallizing requires no curing, so the full metal thickness is applied in one shift and the sealer and paint can follow.
For a Hyderabad site project, a team travels about 570 km from Bengaluru with blasting, arc spray and airless spray equipment, so that a single crew completes blasting, metal spray and paint in one visit. The same systems can also be applied at our facilities in Bengaluru.
- System order
- Blast, metal spray, sealer, paint
- Metal coating
- Zinc or aluminium, 175–200 µm standard
- Airless spray units
- 5, with pressure pots
- Paint agitators
- 5
- Coating checks
- Digital thickness gauges, cross-hatch adhesion tester
- Site conditions
- Psychrometer for humidity and dew point
Frequently Asked Questions
Should a Hyderabad plant specify zinc, aluminium or paint alone?
Is metallizing worthwhile in an inland, dry climate?
What is a duplex system, and when is it required?
Can you coat steel in areas with solvents or flammable vapour?
Do you supply records for our quality file?
Send Details for a Coating Quote
Please share the structure, its dimensions and location, and your planned shutdown window. Our engineers will respond with a recommended method, schedule and quotation.
- Reply within one working day
- Drawings kept confidential
- Email acknowledgement
Thank you. Your enquiry has been received.
One of our engineers will contact you to discuss the requirement. A confirmation has been sent to your email address.