Thermal Spray Coating in Hyderabad
Mythri Metallizing arc sprays zinc and aluminium onto steel at plants around Hyderabad, with a travelling team and its own equipment.
- Zinc, aluminium, zinc-aluminium 85/15
- Arc and flame spray on site
- Site teams with their own equipment
Metal Spray in a Hot, Chemical Region
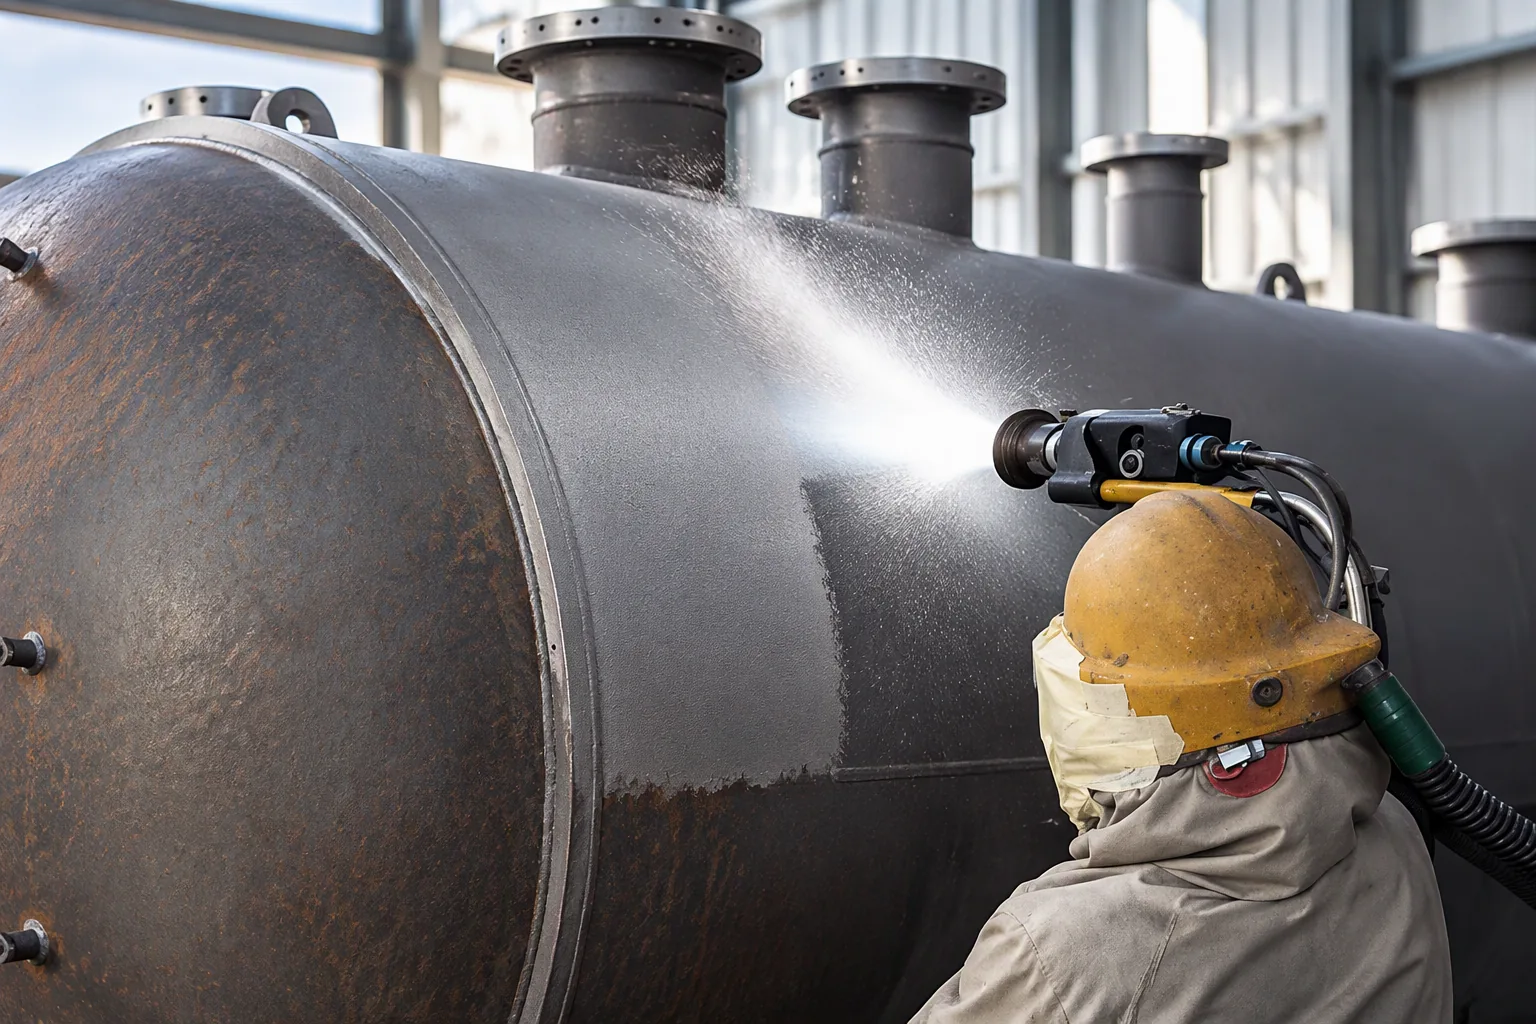
Thermal spray replaces or supports paint where paint struggles. Hyderabad plants present two such conditions: hot surfaces such as boiler and DG chimneys, hot ducts and kiln-area steel, and chemical areas where paint breaks down early.
Aluminium suits the hot surfaces. Aluminium wire of 99.5% purity is arc sprayed onto blasted steel, and a properly applied and sealed coating is expected to last 10 years or more. On preheater structures, rotary kilns and tertiary air ducts, aluminizing can also reduce heat radiation to a certain extent.
Zinc wire of 99.95% purity suits structural steel, tanks and pipe racks in the open. Both coatings are applied cold, so welded and thin sections do not distort and no galvanizing bath limits the size of the structure. The metal is sprayed in place where the structure cannot be moved.
What We Metallize Around Hyderabad
Boiler, DG and process chimneys
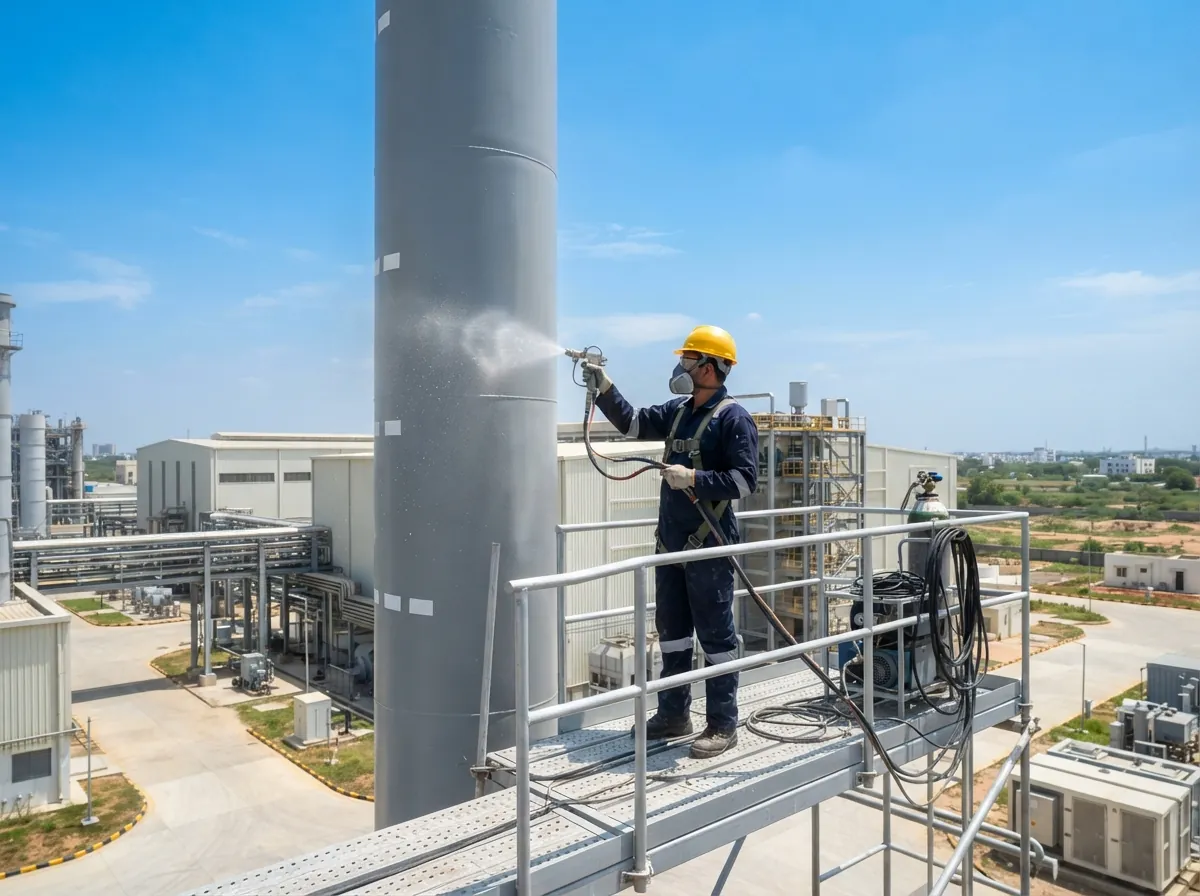
Pharma, bulk drug and power sites operate boilers and DG sets. Chimneys are aluminized in place from scaffolding, usually in a planned shutdown. We have aluminized chimneys in Gujarat, Tamil Nadu and Karnataka.
Cement plant steel
Preheater towers, kiln shells, tertiary air ducts and chimneys at cement plants in the wider region, where aluminizing is applied to the hot zones.
Power equipment and heavy fabrication
Large tanks, frames and structures from the Ramachandrapuram, Balanagar and Medchal belts, metallized in the yard or at the erection site, where a galvanizing bath would limit the size.
Defence, aerospace and engineering parts
Worn shafts and journals are rebuilt by metallizing and machined back to size.
Site Spraying for Hyderabad Plants
For structures at your plant, a team travels about 570 km from Bengaluru with blasting sets, arc spray rectifiers and guns, compressors and airless spray equipment. The site provides access, permits and electrical power for the arc sets. Each section is sprayed within hours of blasting.
Metallizing requires no curing, so the full thickness is applied in one shift and a sealer follows. Thickness is gauged before release and adhesion is tested. Zinc and aluminium coating can also be carried out at our facilities in Bengaluru.
- Arc spray equipment
- 15 rectifier and gun sets
- Wires
- Zinc 99.95% (IS 209), aluminium 99.5%, zinc-aluminium 85/15
- Standard thickness
- 175–200 µm, up to 500 µm possible
- Standards
- Zinc: IS 5905, IS 6586, BS 5493. Aluminium: IS 2590, BS 2569
- Tests
- Thickness to IS 3203, pull-off adhesion to ASTM D4541
Frequently Asked Questions
Can you spray our chimney in place in Hyderabad?
What does our site need to provide?
What temperature can an aluminized surface withstand?
Send a Drawing for a Metallizing Quote
Please share the structure, its dimensions and location, and your planned shutdown window. Our engineers will respond with a recommended method, schedule and quotation.
- Reply within one working day
- Drawings kept confidential
- Email acknowledgement
Thank you. Your enquiry has been received.
One of our engineers will contact you to discuss the requirement. A confirmation has been sent to your email address.